INDUSTRIAL STORAGE SOLUTIONS & CONVEYOR SYSTEMS
Evora Industrial Solutions delivers certified heavy-duty warehouse storage racking and automated material handling conveyor systems engineered for modern manufacturing and logistics hubs.
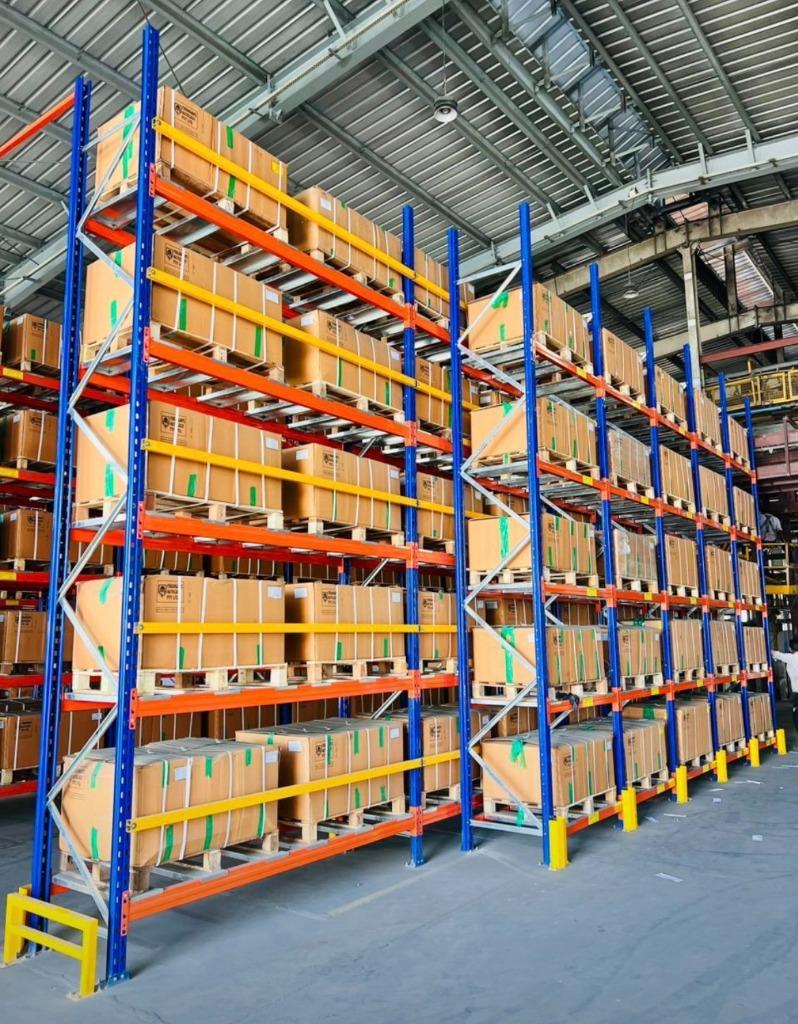
Heavy Duty Pallet Racking Systems
Precision-engineered structural pallet racks designed for high-density warehouse storage, rapid forklift throughput, and maximum cubic space utilization.
INDUSTRIAL STORAGE SOLUTIONS & CONVEYOR SYSTEMS
Evora Industrial Solutions delivers certified heavy-duty warehouse storage racking and automated material handling conveyor systems engineered for modern manufacturing and logistics hubs.
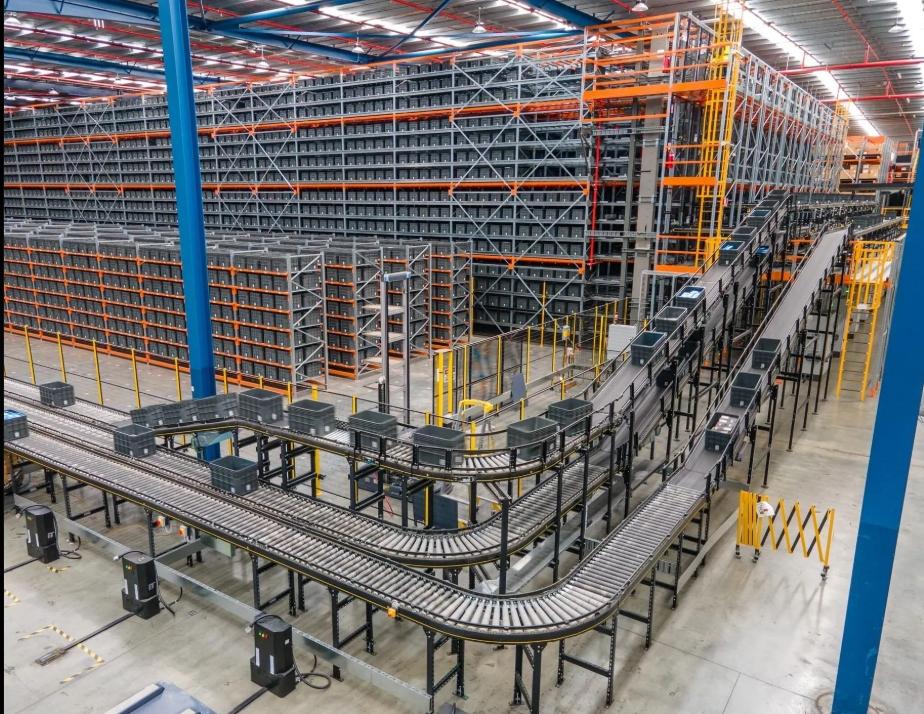
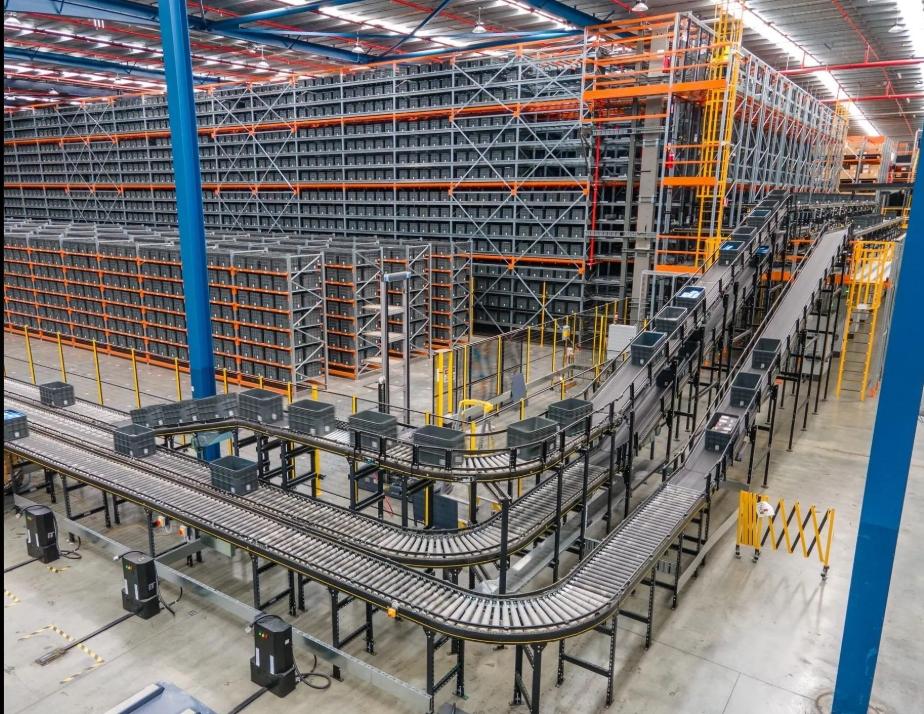
Automated Powered Roller Conveyors
High-speed zero-pressure accumulation motorized roller lines designed for continuous box movement, parcel sorting, and automated fulfillment hubs.
INDUSTRIAL STORAGE SOLUTIONS & CONVEYOR SYSTEMS
Evora Industrial Solutions delivers certified heavy-duty warehouse storage racking and automated material handling conveyor systems engineered for modern manufacturing and logistics hubs.
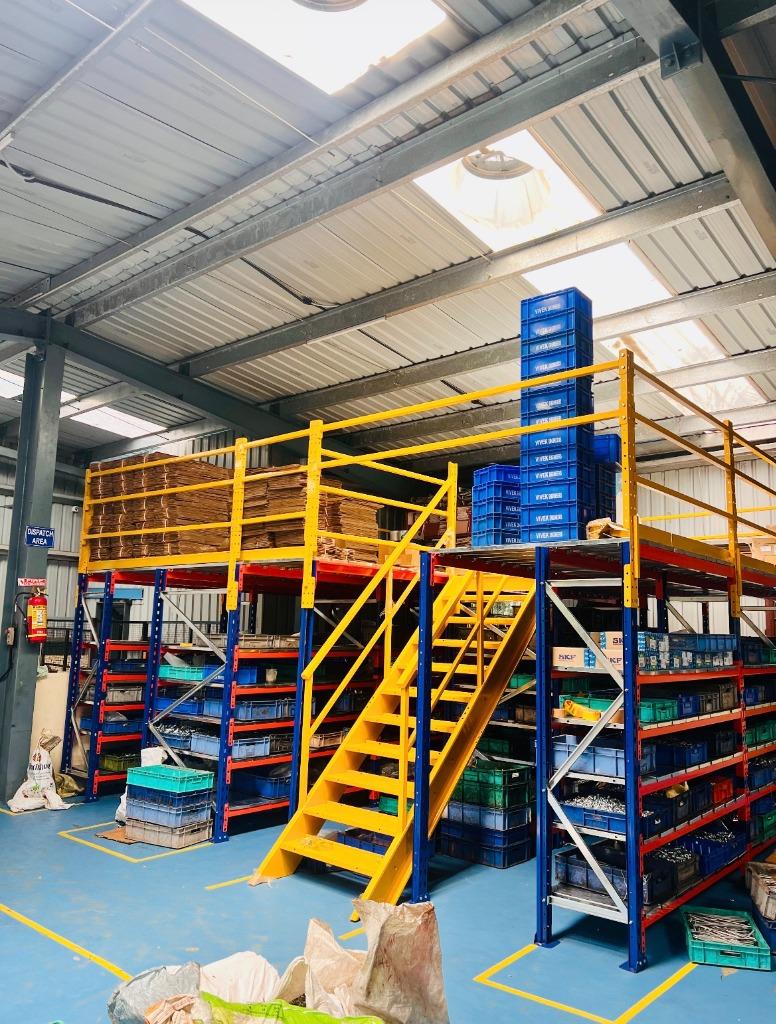
Multi-Tier Mezzanine Floor Systems
Structural steel mezzanine platforms, heavy-duty floor decks, and pick towers that double or triple warehouse cubic capacity without civil construction.
INDUSTRIAL STORAGE SOLUTIONS & CONVEYOR SYSTEMS
Evora Industrial Solutions delivers certified heavy-duty warehouse storage racking and automated material handling conveyor systems engineered for modern manufacturing and logistics hubs.
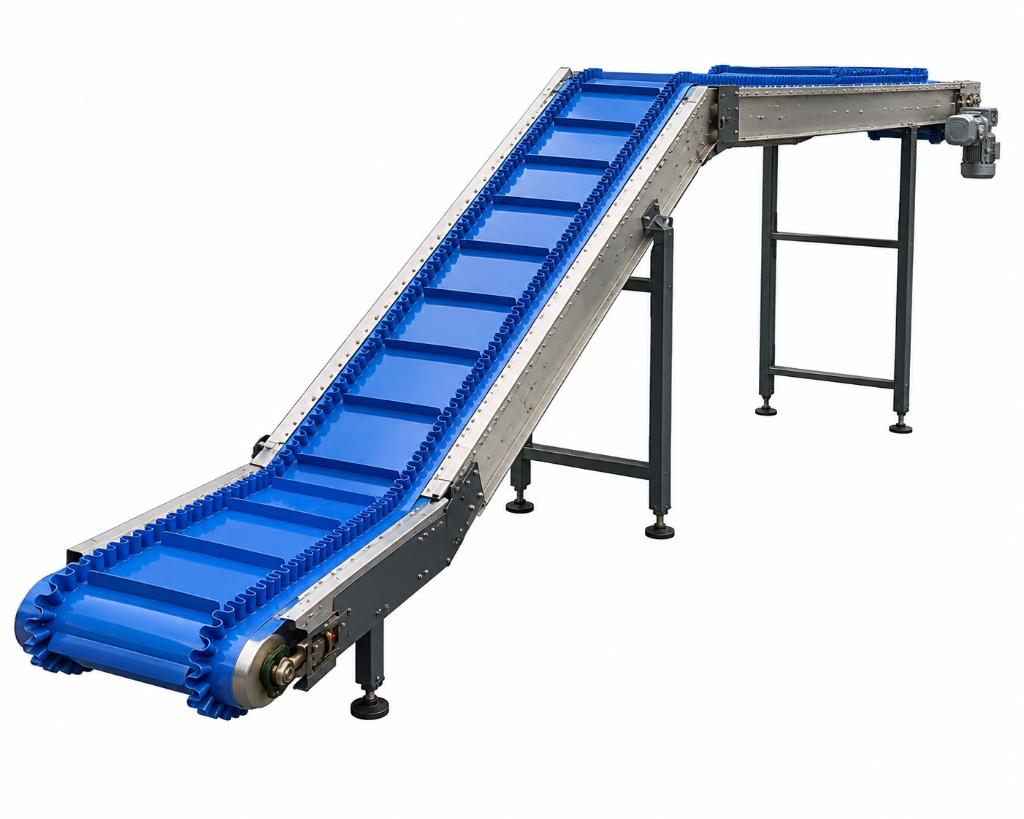
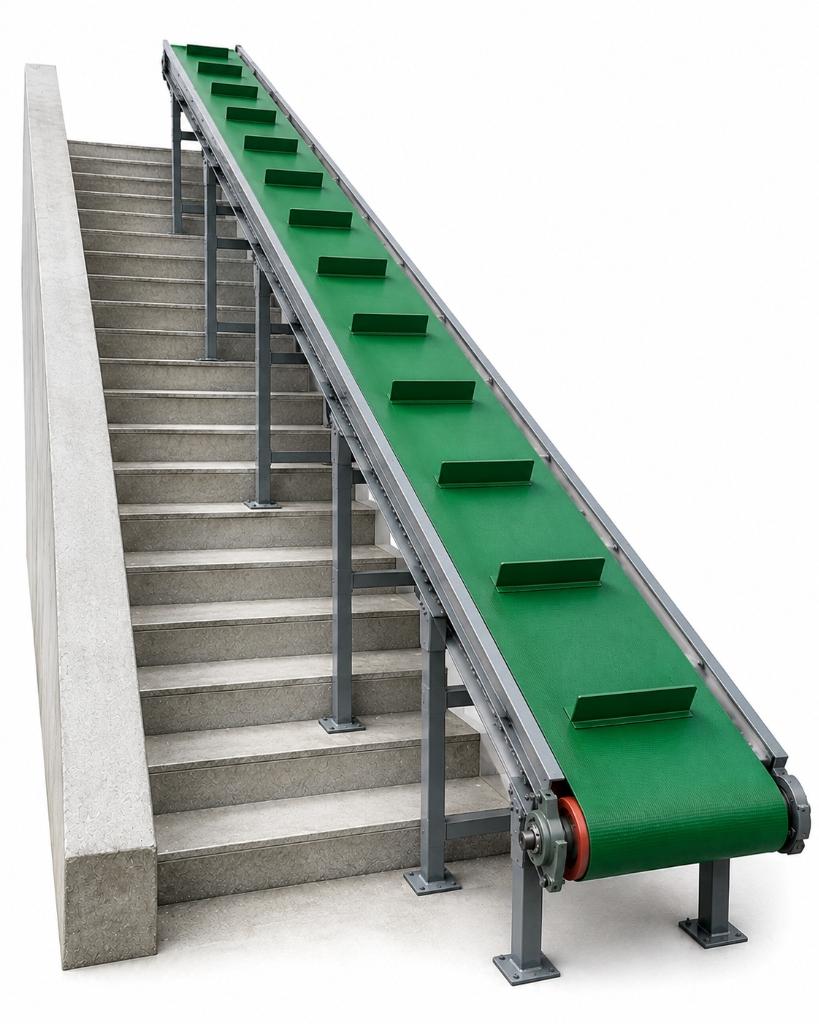
Z-Type Cleated Incline Belt Conveyors
Custom-built swan-neck inclined conveyors with hot-welded cleats and corrugated sidewalls for floor-to-floor bulk parts and package elevation.
INDUSTRIAL STORAGE SOLUTIONS & CONVEYOR SYSTEMS
Evora Industrial Solutions delivers certified heavy-duty warehouse storage racking and automated material handling conveyor systems engineered for modern manufacturing and logistics hubs.
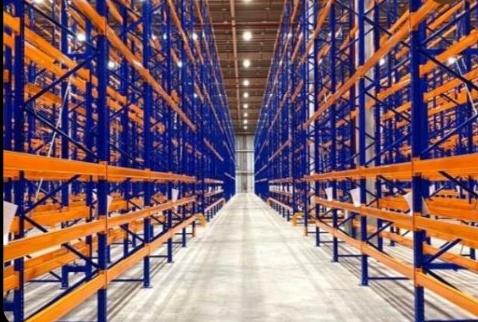
Heavy Duty Cantilever Racking Systems
Unobstructed horizontal storage frameworks engineered for certified load-bearing storage of steel pipes, timber, extrusions, and heavy bars.
INDUSTRIAL STORAGE SOLUTIONS & CONVEYOR SYSTEMS
Evora Industrial Solutions delivers certified heavy-duty warehouse storage racking and automated material handling conveyor systems engineered for modern manufacturing and logistics hubs.
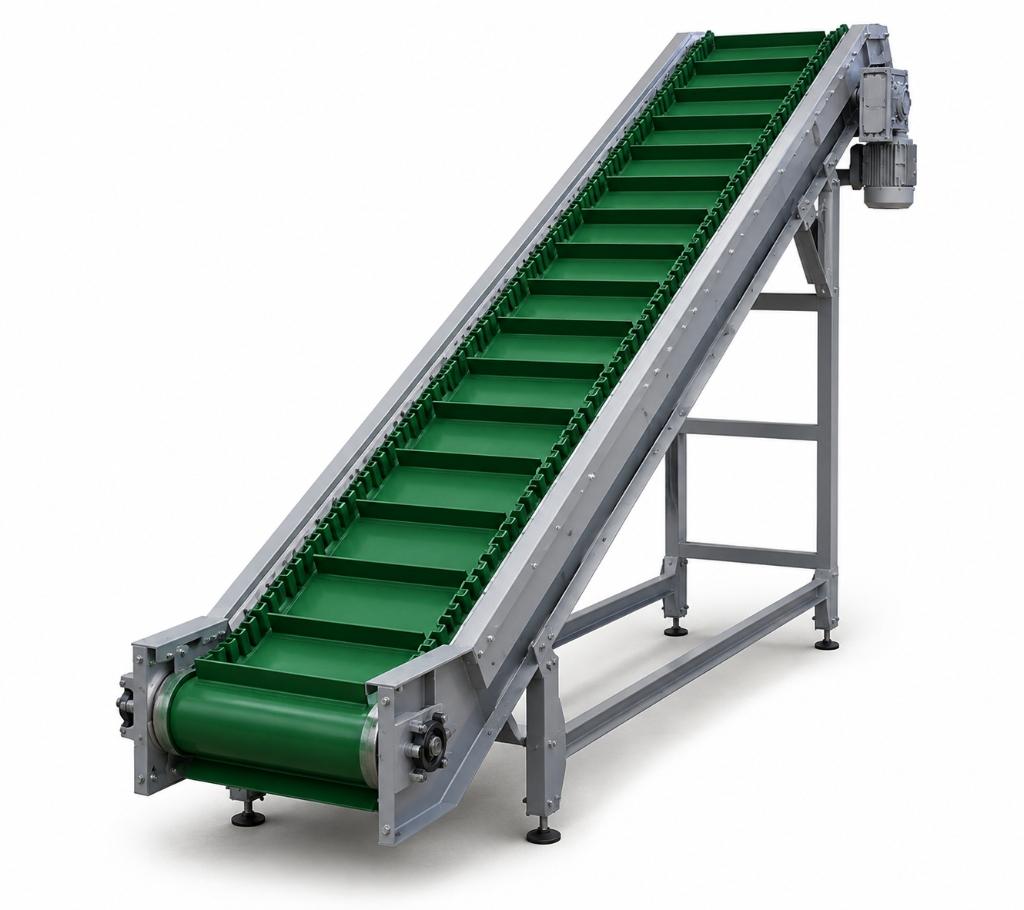
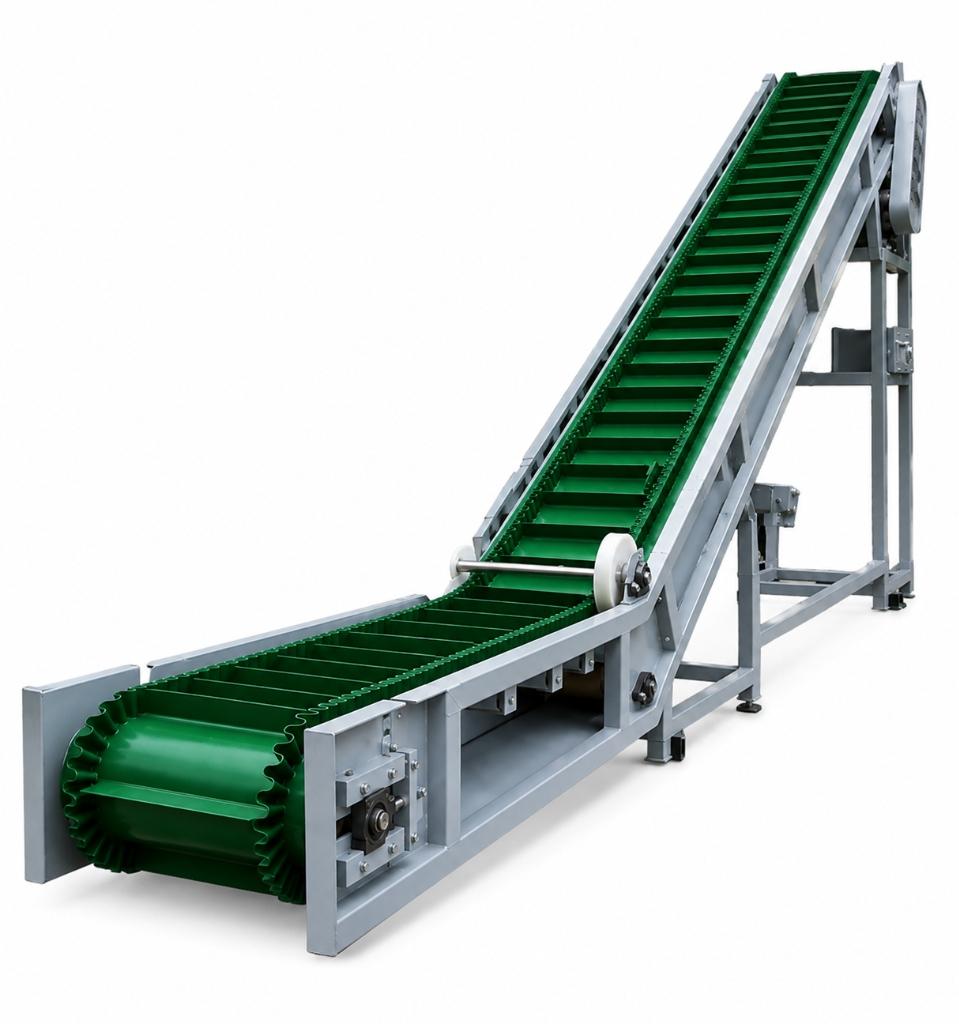
Steep Incline Corrugated Sidewall Conveyors
Cross-rigid base belt conveyors with high-angle corrugated sidewalls for steep space-constrained bulk material elevation without material rollback.
Industrial Storage Solutions & Conveyor Systems
Evora Industrial Solutions is an industrial engineering and manufacturing enterprise specializing in high-density warehouse storage systems and automated material handling conveyor networks.
We help logistics distribution hubs, manufacturing plants, automotive assembly units, and e-commerce facilities double their cubic storage volume while accelerating continuous material throughput.
Industrial Storage Systems
- • Heavy Duty Pallet Racking
- • Multi-Tier Mezzanine Floors
- • Cantilever Racks & Long Span
Industrial Conveyor Systems
- • Powered Roller Lines (ZPA)
- • Cleated Z-Incline Belt Elevators
- • Assembly & Sorting Conveyors
Industrial Storage Systems & Conveyor Lines
From high-density structural pallet racking to automated motorized conveyor networks, we engineer and manufacture complete material handling infrastructure to European standards.
Heavy Duty Pallet Racking
High-density selective pallet racking, cantilever systems, drive-in racking, and heavy duty shelving engineered for maximum warehouse storage density.
Powered & Roller Conveyors
Automated motor-driven roller conveyors, zero-pressure accumulation lines, and gravity roller beds built for continuous box movement and distribution logistics.
Multi-Tier Mezzanine Floors
Heavy-duty structural steel mezzanine platforms, pick towers, and multi-tier storage decks that double or triple warehouse cubic capacity without civil work.
Incline & Cleated Belt Conveyors
Z-type swan-neck conveyors, steep incline corrugated sidewall belts, and modular belt assembly lines for floor-to-floor elevation and continuous production flow.
Why Choose Evora Industrial Solutions
Delivering robust mechanical engineering, high-density storage frameworks, and dependable conveyor systems engineered for heavy-duty industrial operations.
Structural Storage Engineering
Precision structural calculations, certified high-tensile steel roll-forming, and beam safety locking pins engineered for high-density pallet and cantilever storage.
Automated Conveyor Networks
High-speed zero-pressure accumulation roller lines, cleated incline elevators, and modular belt systems designed for continuous, safe material handling.
Customized Facility Layouts
Bespoke racking heights, custom conveyor belt widths, adjustable pitch mezzanine platforms, and tailored material handling configurations.
Cubic Volume & Flow Optimization
Engineering solutions designed to double vertical warehouse storage footprint while accelerating material transit throughput between production zones.
Quality-Oriented Manufacturing
Certified raw materials, precision CNC punching, automated roll-forming lines, and electrostatic powder coating built for rugged 24/7 industrial life cycles.
Turnkey Installation & Support
Comprehensive lifecycle support including expert on-site erection, optical laser alignment, load deflection testing, and prompt preventive maintenance.
Industries We Serve
Tailored storage architectures and material conveyance solutions engineered for demanding operational environments across diverse industrial sectors.
Warehousing & Distribution
High-density pallet racking, carton flow picking systems, and sortation conveyors for rapid fulfillment.
Manufacturing Plants
Assembly line belt conveyors, powered roller networks, and heavy tooling storage racks built for 24/7 duty.
Logistics & Supply Chain
High-throughput cross-docking roller conveyors, truck loading/unloading lines, and dispatch storage.
Automotive Industry
Heavy-duty cantilever racks, slat & chain conveyors, and specialized engine/body panel handling systems.
Food & Beverage
Food-grade washdown modular belt conveyors and galvanized cold-storage drive-in pallet racking.
Pharmaceutical Industry
Clean-room modular conveyors, stainless steel roller systems, and secure multi-tier shelving archives.
Engineering & Industrial Facilities
Structural steel mezzanine floors, die and mould storage racks, and overhead/floor material transfer units.
Engineered Storage Solutions & Conveyor Systems
Explore our balanced portfolio of certified heavy-duty pallet racking, structural mezzanine floors, motorized roller conveyors, and cleated incline elevators designed for modern industrial operations.
Our Work Process
A disciplined, engineering-first project lifecycle ensuring precision, compliance, safety, and on-time commissioning.
Requirement Understanding
Detailed analysis of your warehouse inventory profile, throughput targets, payload weights, and material handling objectives.
Site Assessment
Physical site surveying, floor slab load verification, column grid measurement, and vertical clear headroom mapping.
Engineering & Design
Developing optimal CAD layouts, 3D structural simulations, conveyor velocity calculations, and customized storage density plans.
Manufacturing
Precision structural fabrication using certified high-tensile steel, CNC roll-forming, and high-adhesion powder coating.
Installation
Professional on-site erection, optical laser alignment, electrical drive integration, and rigorous full-load testing.
Support
Comprehensive handover, operator safety guidelines, routine preventive maintenance, and prompt technical support.