Multi-Tier Mezzanine Storage System
Introduction
About Multi-Tier Mezzanine Storage System
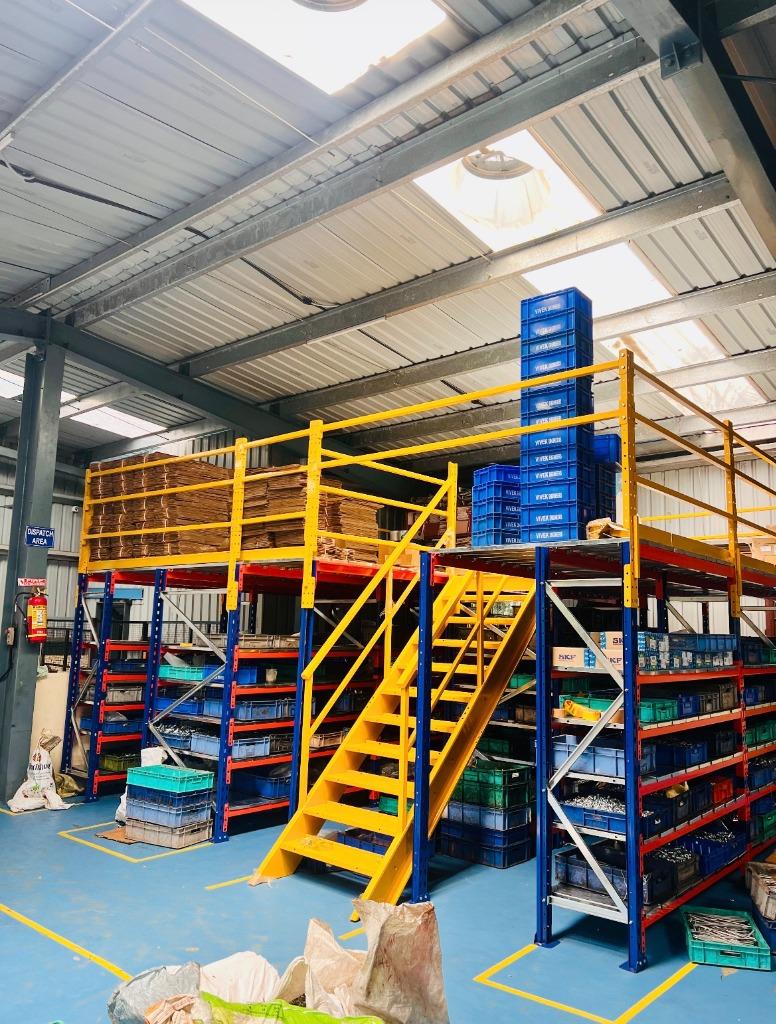
Multi-Tier Mezzanine Storage System is a premium Mezzanine Floors solution engineered to deliver reliable performance, structural safety and long-term durability for warehouses, manufacturing plants, and distribution centers. It is manufactured using high-grade certified materials to ensure high load capacity and smooth operation even in demanding industrial environments.
At Evora Solutions, we provide complete design, fabrication, installation, load testing and after-sales support for Multi-Tier Mezzanine Storage System. Every system is tailored according to the customer's facility dimensions and operational requirements to achieve maximum storage density and material handling speed.
Our storage and conveyor systems are widely deployed in manufacturing facilities, warehouses, logistics parks, automotive plants, e-commerce centers, and cold storage facilities across Pune, Maharashtra and India. We focus on delivering durable, space-optimizing industrial solutions backed by dedicated engineering support.
Why Choose Multi-Tier Mezzanine Storage System?
Our Multi-Tier Mezzanine Storage System systems are engineered to deliver high load durability, space efficiency, and long-term performance for industrial storage and conveyor applications.
Enhanced Safety
Designed to improve operational safety with reliable automation.
High Performance
Smooth and efficient operation with consistent long-term performance.
Easy Operation
Simple to use with user-friendly controls and automation features.
Low Maintenance
Built using premium quality components for minimum maintenance.
Long Service Life
Engineered for durability even in demanding industrial environments.
Professional Installation
Complete installation, load testing and technical support by Evora Solutions.
Frequently Asked Questions
Request Product Enquiry
Tell us about your requirement. Our Evora Solutions specialists will contact you with the best solution for your application.
Technical Specifications
| Safety | Staircase with safety yellow handrails and kickplates |
| Structure | Heavy-duty roll-formed / I-beam steel framework |
| Decking Options | Chequered plate, galvanized grating, or heavy particle board |
| Floor Load Capacity | 300 to 1,500 kg / sqm |
Key Features
Designed for reliable industrial storage and conveyor performance by Evora Industrial Solutions.
Applications
Suitable for multiple industrial environments.
Spare Parts & Hardware Distribution
E-Commerce Order Fulfillment Centers
Assembly Workshops & Office Mezzanines